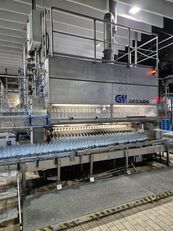
ماكينة تنظيف العبوات KHS Blomax 16


 Wentorf bei Hamburg

إذا قررت شراء المعدات بسعر منخفض، فتأكد أنك تتواصل مع البائع الحقيقي. اكتشف أكبر قدر ممكن من المعلومات عن مالك المعدات. تتمثل إحدى طرق الغش في تقديم نفسك كشركة حقيقية. إن ساورك شك، أخبرنا عن ذلك من أجل تشديد الرقابة وذلك من خلال نموذج التعليقات.
قبل أن تقرر القيام بالشراء، احرص على مراجعة العديد من عروض البيع بعناية لفهم متوسط تكلفة المعدات التي اخترتها. إذا كان سعر العرض الذي أعجبك أقل بكثير من عروض مشابهة، ففكر في الأمر بتأنٍ. قد يكون هناك فرق أسعار هائل يشير إلى عيوب مخفية أو أن البائع يحاول ارتكاب أعمال احتيالية.
ابتعد عن شراء المنتجات التي يكون سعرها مختلف بشدة عن متوسط السعر لمعدات مشابهة.
لا توافق على الوعود المثيرة للشكوك والبضائع المدفوعة مسبقًا. إن ساورك شك، فلا تخاف من طلب توضيح التفاصيل وأن تطلب صورًا ومستندات إضافية للمعدات وأن تفحص صحة التصديق على تلك المستندات وتطرح الأسئلة التي تساورك.
أكثر أنواع الاحتيال شيوعًا، قد يطلب البائعون غير المنصفون مبلغًا معينًا كعربون مسبق "لتحجز" حقك في شراء المعدات. وبالتالي يستطيع المحتالون تجميع مبلغًا ضخمًا ثم يختفون ولا تستطيع التواصل معهم بعد ذلك.
- إرسال الدفعة المسبقة إلى البطاقة
- لا تقم بالدفع المسبق بدون مستندات ورقية تؤكد عملية تحويل الأمول إذا ساورك أي شك في البائع خلال التواصل.
- إرسال إلى حساب "الوصي" “Trustee”
- هذا الطلب ينبغي أن يكون بمثابه إنذار فأنت على الأرجح تتواصل مع شخص محتال.
- إرسال إلى حساب الشركة باسم مشابه
- توخّ الحذر، فقد يختفي المحتالون أنفسهم أيضًا خلف شركات معلومة أو يدخلون تغييرات طفيفة على الاسم. لا تحول الأموال إذا ساورك شك في اسم الشركة.
- استبدال البيانات الخاصة في فاتورة شركة حقيقية
- قبل التحويل، تأكد أن البيانات المحددة صحيحة وأنها ترتبط أو لا ترتبط بالشركة المحددة.
معلومات الاتصال بالبائع


 ألمانيا، Menslage

 ألمانيا، Burgwald-Ernsthausen


 ألمانيا، Menslage


 ألمانيا، Burgwald-Ernsthausen


 ألمانيا، Menslage


 ألمانيا، Burgwald-Ernsthausen


 ألمانيا، Burgwald-Ernsthausen


 ألمانيا، Burgwald-Ernsthausen


 ألمانيا، Burgwald-Ernsthausen


 ألمانيا، Burgwald-Ernsthausen


 ألمانيا، Burgwald-Ernsthausen


 ألمانيا، Menslage


Capacity: 28.800 bottles/h
Bottle size: min. 200 ml and max. 2.000 ml
Bottle neck nominal diameter: 38 mm
Production hours: 24.288 hours
Electrics: 380 V - 50 Hz - 3 pH - Earth
Space requirement: 11,60 x 10,60 x 3,10 meter
Nettogewicht: ± 27.500 kg
On behalf of our client
we are selling this KHS Blomax 16 PET blow molding machine which is designed for the automated production of PET bottles. It ran together with 2x KHS Absofill / ABF 710 machines before (one of these 2 also sold by our website
إظهار قائمة الأسماء It is dismantled ± 8 years ago and is stored since in a closed warehouse. The client bought the machine used and decided not to blow bottles themselve
but buy them from another supplier
already blown. This bottle blower is direct available. Loading on the truck / inside the container will be done by the dairy factory.The machine was used to blow PET bottle for a fruit juice factory in Germany. Capacity: 28.800 bottles/h. Bottle size: min. 200 ml and max. 2.000 ml. Current bottle neck nominal diameter: 38 mm. With the same nominal bottle neck diameter
different bottles shapes and sizes can be blown. Max diameter of the bottle: 115 mm. Length of the bottle: min: 107 mm and max. 350 mm. Length of the prefrom: min. 60 mm and max. 185 mm. Power: 400 V - 3 Ph - 50 Hz - ± 300 kW. Total dimensions: ± 930 x 520 x 310 cm. Space requirement (length x width): 11,60 x 10,60 meter. Weight:± 27.500 kg.Working principle: The preforms are located in the feed hopper of the inclined conveyor. From here
they are transported to the roller sorter
which aligns the preforms. The preforms are transported via the feed rails to the loading station. Here
they are conveyed to the preform turner. The preform turner takes the preforms individually
turns them
and transfers them to the grippers of the loading station. The loading station places one preform at a time on a transport mandrel of the loading/unloading wheel. From here
the preforms – mounted on transport mandrels – pass through the machine. The preform or the produced bottle remains on the transport mandrel throughout the entire machine cycle. Transfer station I guides the transport mandrels with the preforms placed on them onto the mandrel holders of the linear furnace. Heating boxes with infrared heaters are housed in the linear furnace. At the end of the heating section
a pyrometer approximately 35 mm above the support ring non-contacts the temperature of the preforms. From the heating section
the preforms are transferred from transfer station II to the blow molding stations on the blow molding wheel. The movements of the blow molding station are
opening/closing the blow mold
raising/lowering the base mold
raising/lowering the stretching rod
raising/lowering the blow nozzle are controlled by cams. The "Lock mold" and "Unlock mold" curves are adjustable. The blow molding process consists of the stretching process and a two-stage blow molding process. The first pressure stage (P1) is used to blow the bottle
while the second
higher pressure stage (P2) is used to shape the bottle contour and press the bottle wall against the mold. By utilizing the AR blow air recirculation (AIRBACK®) – which serves to save blow air – the blow molding process proceeds. After the blow molding process is complete
the molds open
and Transfer Station III conveys the transport mandrels containing the finished bottles to the loading/unloading wheel. From here
the bottles enter the bottle turning wheel. Here
they are picked up by grippers
and the transport mandrels are released. From the bottle turning wheel
the bottles are suspended on guide rails and transported out of the machine area by air.Additional features:The touchscreen operation panel is missing.Currently no photos available of the feed hopper and the inclined conveyor for the preforms
but these items are included in the quotation.Including Riedel cooling system
PC1601S1M496654
Refrigerant R407C